Construction and service duty
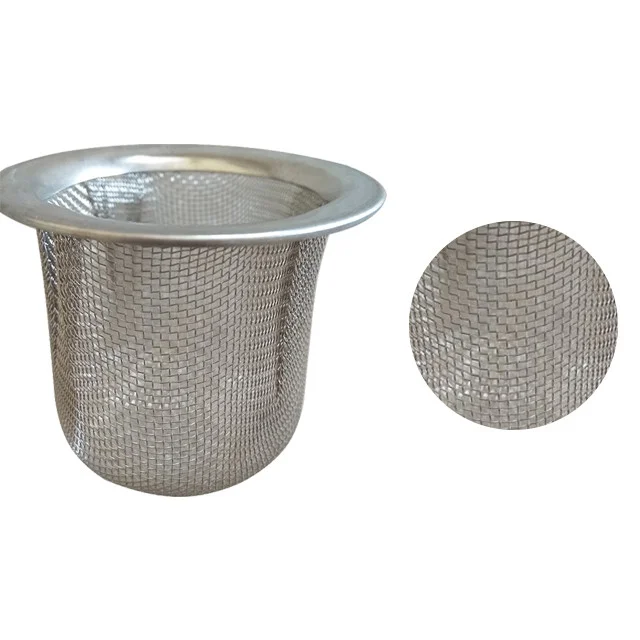
Pressed mesh cup with an integral seating flange. Pressed or drawn mesh cups introduce a controlled depth in a small envelope. Forming can change aperture and wall thickness locally, so finished-part inspection matters.
Pressed mesh cup with an integral seating flange.
Metal wire meshShare a drawing, reference sample or application requirements to discuss the configuration.
Flanged filter cups
| Parameter | Specification | Notes |
|---|---|---|
| Media / opening | Mesh grade and formed aperture to verify | Typical enquiry information; final rating requires agreement. |
| Dimensions | Flange OD / body depth to drawing | Manufactured to the approved drawing. |
| End connection / assembly | Flange flatness and edge finish to specify | Confirm the interface on the assembly drawing. |
| Common alloys | Stainless steel 304 or 316L; other grades by drawing | Provide depth, flange width, corner radius and seating detail. |
| Drawing dimensions | Flange OD / body depth to drawing | — |
Materials: Stainless steel 304 or 316L; other grades by drawing
Pressed mesh cup with an integral seating flange. Pressed or drawn mesh cups introduce a controlled depth in a small envelope. Forming can change aperture and wall thickness locally, so finished-part inspection matters.
Pressed or drawn mesh cups introduce a controlled depth in a small envelope. Forming can change aperture and wall thickness locally, so finished-part inspection matters.

Push-fit filter inserts and Washable inlet screens. Confirm the operating fluid, flow direction, temperature and allowable pressure differential before selecting this construction.
Specify the mating component and process conditions for push-fit filter inserts.
Check installation, cleaning and service access for washable inlet screens.
Include these details when discussing your requirements.
Send a drawing or reference sample, mesh grade and formed aperture to verify, flange od / body depth to drawing, flange flatness and edge finish to specify, quantity and intended service.
The starting media is only one input; inspect the formed geometry and aperture where the forming strain is highest.
Explore related products and technical guidance.
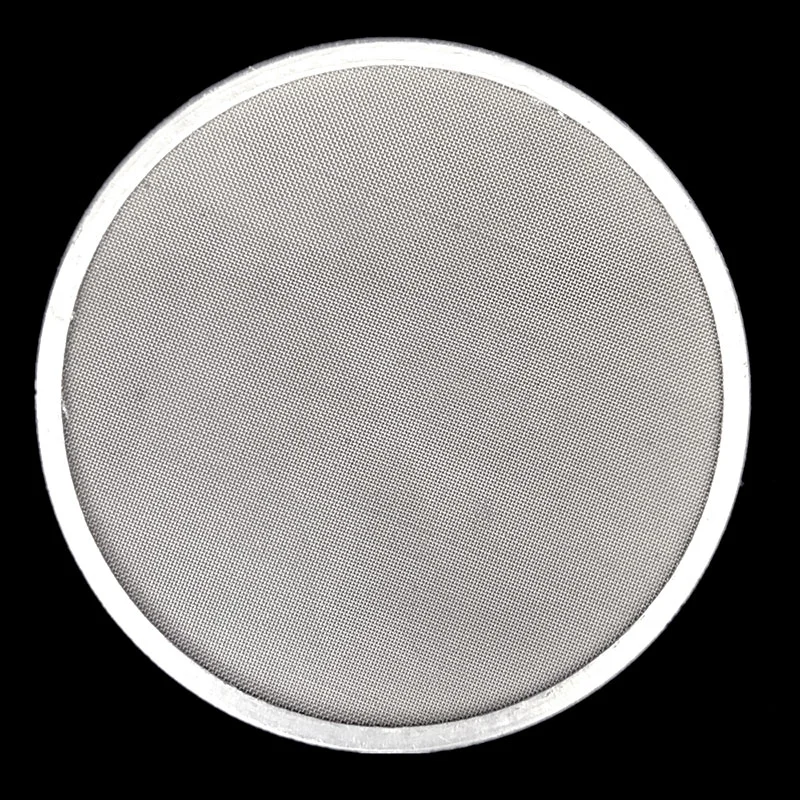
Mesh disc with retained metal perimeter for repeated handling.
View details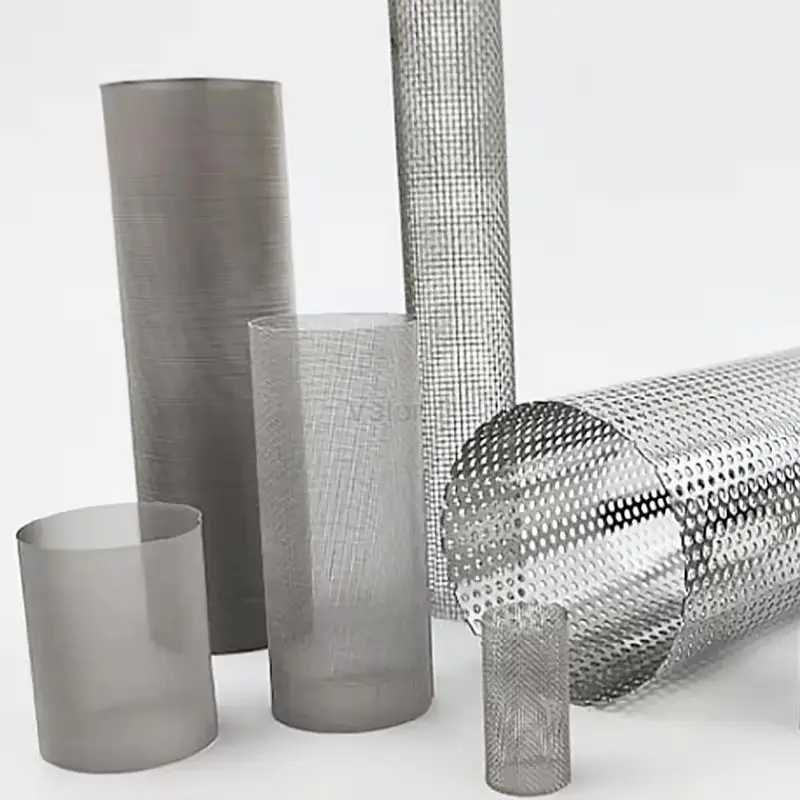
Open-ended welded mesh cylinder for removable screens and pump protection.
View details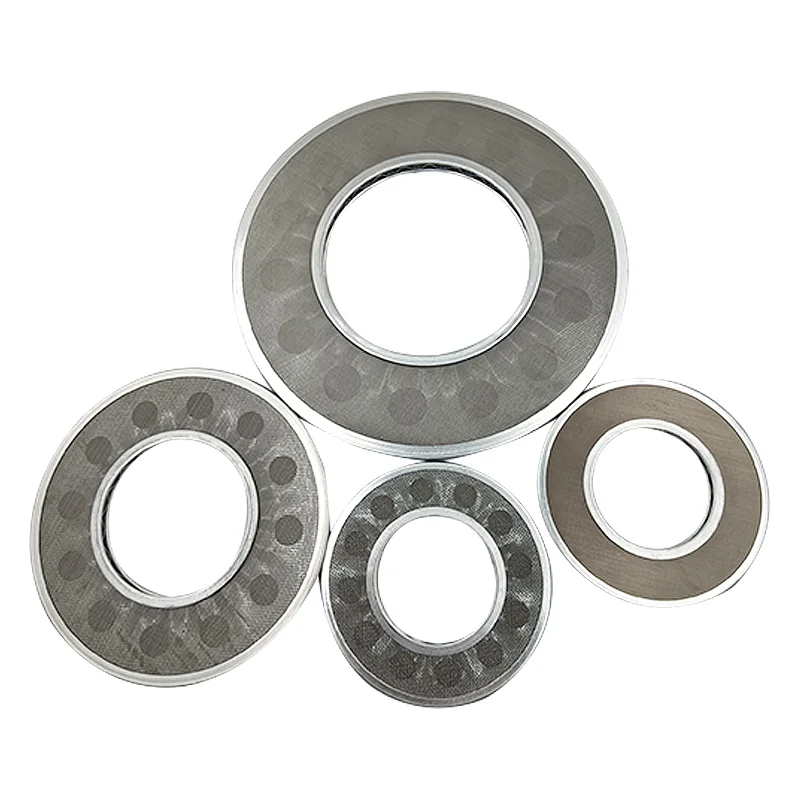
Ring-shaped mesh disc for an annular seat or central feed passage.
View detailsDefine the dimensions, media, joints and inspection records before confirming the order.