Project requirement
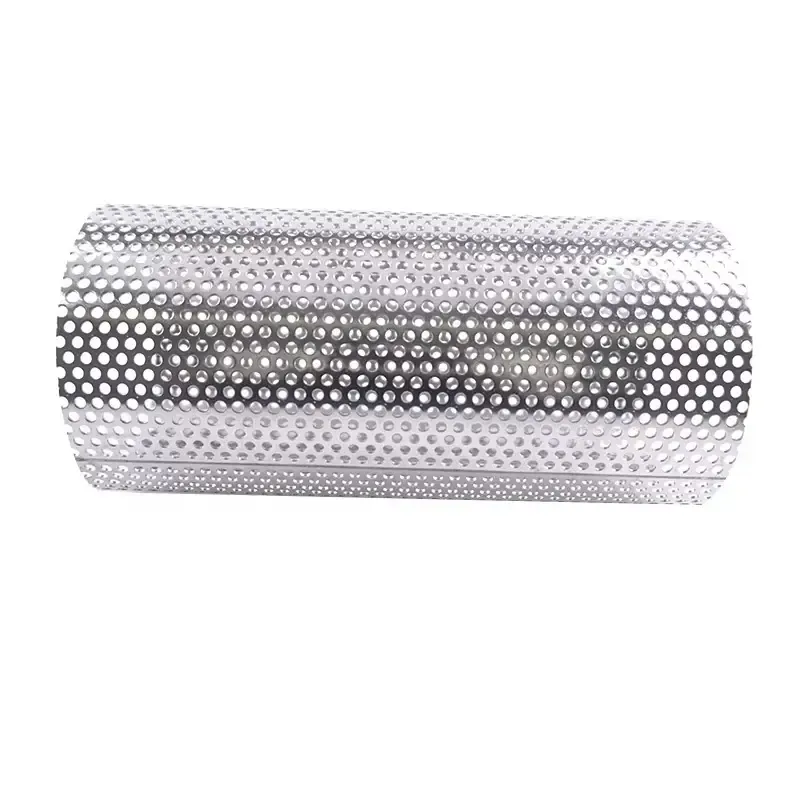
A Bulgarian food-equipment project called for a perforated filter element with 0.8 mm holes. The customer wanted an approximately 2 mm area without holes on each side of the weld. That margin changes the flat perforation layout and the location of the closing seam.
Engineering question
If perforations extend into the weld zone, the seam can become irregular and the finished cylinder can lose a controlled joint line. The drawing review should set the hole field, blank margin, forming direction and weld location before production. The 2 mm value should be treated as a specified target until the customer approves the flat pattern and tolerances.
Project status
The custom perforated, welded element was delivered. The case describes the specified solid welding margin without claiming unprovided inspection measurements.
Design review
The roughly 2 mm unperforated area beside the weld should be drawn into the flat pattern before forming. Hole pitch, seam position and final diameter interact; moving the seam after perforation can change both strength and the visible pattern. The 0.8 mm hole callout should remain separate from any filtration-efficiency claim.
Inspection and acceptance
The custom welded element was delivered. The case documents a specified weld-margin concept but contains no measured seam-strength or hole-tolerance report. Agree inspection points on the approved drawing for a repeat or scale-up order.